
Quality control steps
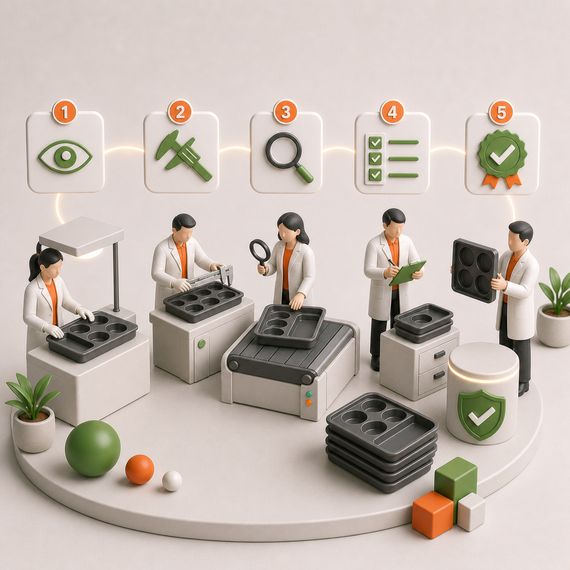
Each stage of coating inspection answers a different question. The soundness of the body, surface preparation, application distribution, and operating result are not the same check. In Powerpan assessments, the inspection scope should be defined according to the part and selected system.
New parts and used equipment also have different starting conditions. Refurbishment includes examination of the old layer’s condition and the metal surface after removal. If cracks, corrosion, or deformation are present, the work scope is reassessed.
Before and during application
Areas to be coated, surfaces to be protected, and critical dimensions should be defined. Internal corners, deep grooves, and assembly points require separate attention. The surface preparation method selected is checked for suitability to the base material.
During application, layer distribution and thickness are compared with the relevant system’s information. Wet- and dry-film inspection are not the same assessment; the method and measurement location should be selected appropriately. The same device or measurement plan must not be assumed to apply to every surface.
Curing and final inspection
Curing conditions are based on the system instructions. The process temperature must not be confused with the equipment’s end-use temperature. Affected parts should be identified in a batch with a deviation; the correction method should be selected through technical assessment.
| Inspection topic | Information needed for a decision |
|---|---|
| Body | Damage and suitability for reuse |
| Coating | Defined surface and thickness criteria |
| Assembly | Dimensional and movement compatibility |
| Use | Functional assessment under actual conditions |
Visual inspection does not replace adhesion or thickness checks. The methods and acceptance criteria for the required tests should be defined at the start of the project. If a product operating trial is needed, its conditions are also recorded.
Linking batch identity to results makes the delivery decision clear. A nonconforming part should be segregated and must not be returned to service or released for delivery before the correction has been checked. The inspection and reporting scope is confirmed separately during quotation discussions with Powerpan. Requests for food-contact documents or corporate certificates must not be confused with final inspection records. If the recipe or operating conditions change after delivery, the previous result may no longer be accepted within the same scope.